 YokoGawa Pressure Transmitters
 ABB Pressure Transmitters
 E+H Pressure Transmitters
 WIKA
 HoneyWell Pressure Transmitters
 Micro Motion Coriolis
 Rosemount Flow Meters
 YokoGawa Flow Meters
 E&H Flow Meters

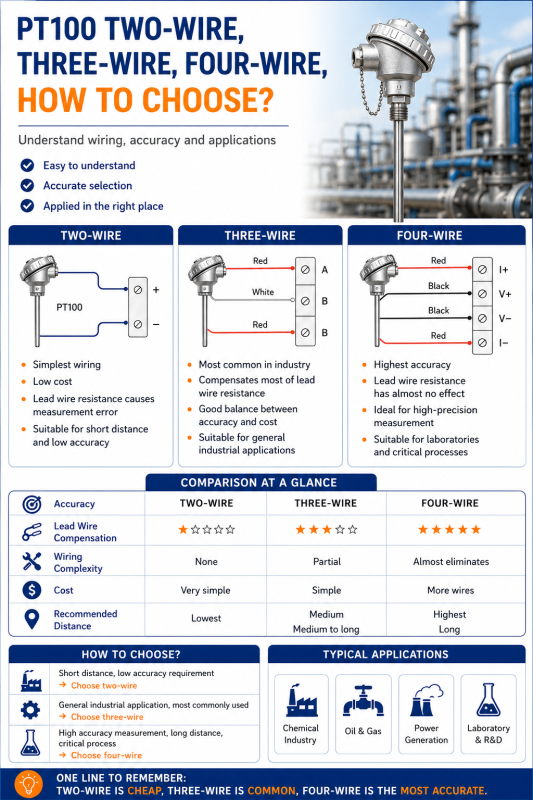
PT100 resistance temperature detectors are widely used in industrial temperature measurement.
However, many users become confused when selecting between two-wire, three-wire and four-wire PT100 sensors.
All three configurations use the same basic PT100 sensing element, but their wiring methods, measurement accuracy, installation cost and suitable applications are different.
The correct choice should not be based only on whether the sensor can connect to the instrument. You should also consider:
- Required measurement accuracy
- Cable length
- Lead wire resistance
- Installation cost
- PLC, DCS or transmitter input type
- Actual process conditions
In simple terms:
Two-wire is economical, three-wire is the industrial standard, and four-wire provides the highest accuracy.

What Is a PT100 Temperature Sensor?
A PT100 is a platinum resistance temperature detector, also known as an RTD.
The term “PT100” means that the sensing element has a nominal resistance of approximately 100 ohms at 0°C.
As the temperature increases, the resistance of the platinum element also increases.
The connected transmitter, PLC, DCS or temperature indicator measures this resistance and converts it into a temperature value.
The main difference between two-wire, three-wire and four-wire PT100 sensors is not the sensing element itself.
The difference is how the measurement system handles the resistance of the connecting wires.
Why Does Lead Wire Resistance Affect PT100 Accuracy?
A PT100 measuring circuit does not only measure the resistance of the sensing element.
Depending on the wiring method, it may also measure part or all of the resistance from the lead wires.
The measured resistance can be expressed as:
Measured resistance = PT100 sensor resistance + lead wire resistance
The longer and thinner the cable is, the higher its resistance will be.
This additional resistance can make the instrument calculate a temperature that is higher than the actual process temperature.
For example, if the sensor is installed far from the control cabinet, the cable resistance may become large enough to create a noticeable temperature error.
This is why wiring selection becomes more important as the cable distance and accuracy requirements increase.
PT100 Two-Wire Connection
A two-wire PT100 has one wire connected to each side of the sensing element.
It is the simplest and lowest-cost wiring method.
However, the resistance of both lead wires is added directly to the PT100 resistance measurement.
Advantages of a Two-Wire PT100
- Simple wiring
- Lowest sensor and cable cost
- Easy to install
- Requires only two input terminals
- Suitable for short cable distances
Limitations of a Two-Wire PT100
- Lead wire resistance directly creates measurement error
- Error increases as the cable becomes longer
- Not suitable for high-accuracy measurements
- Cable size and ambient temperature can affect the result
When Should You Use a Two-Wire PT100?
A two-wire PT100 may be suitable when:
- The cable distance is short
- Measurement accuracy is not critical
- The installation budget is limited
- The sensor is used for basic equipment monitoring
- The input device only supports a two-wire resistance input
- A temperature transmitter is installed close to the sensor
A two-wire PT100 is often used in general machinery, HVAC systems and low-cost equipment monitoring.
PT100 Three-Wire Connection
A three-wire PT100 uses two wires on one side of the sensing element and one wire on the other side.
It is the most commonly used configuration in industrial plants.
The measuring instrument uses the third wire to estimate and compensate for most of the lead wire resistance.
This compensation normally assumes that the two matching lead wires have approximately the same resistance.
Advantages of a Three-Wire PT100
- Compensates for most lead wire resistance
- Better accuracy than a two-wire connection
- Lower cost than a four-wire system
- Widely supported by PLCs, DCS systems and temperature transmitters
- Suitable for most industrial applications
Limitations of a Three-Wire PT100
- Compensation is based on matching lead wire resistance
- Unequal wire lengths or conductor sizes can create residual error
- Less accurate than a four-wire measurement
- Incorrect terminal wiring can produce unstable readings
When Should You Use a Three-Wire PT100?
A three-wire PT100 is generally the best choice when:
- The sensor is installed in a normal industrial process
- Medium or long cable distances are required
- Good accuracy is needed without excessive cost
- The PLC, DCS or transmitter supports three-wire RTD input
- The installation is used in oil and gas, chemical, power or water treatment applications
For most industrial users, three-wire is the standard and most practical selection.
PT100 Four-Wire Connection
A four-wire PT100 uses two wires to supply the measuring current and two separate wires to measure the voltage across the sensor.
Because the voltage measurement circuit draws almost no current, the resistance of the voltage wires has very little effect on the final reading.
This method can almost completely eliminate lead wire resistance error.
Advantages of a Four-Wire PT100
- Highest measurement accuracy
- Almost eliminates lead wire resistance error
- Suitable for long cable distances
- Ideal for calibration and reference measurements
- Does not depend on perfectly matched lead wire resistance
Limitations of a Four-Wire PT100
- Higher sensor and cable cost
- Requires more terminals
- More complex installation
- Not all PLC or DCS input modules support four-wire RTDs
- May provide little practical benefit in low-accuracy processes
When Should You Use a Four-Wire PT100?
A four-wire PT100 is recommended for:
- Laboratory temperature measurement
- Calibration systems
- High-accuracy test equipment
- Critical process control points
- Long-distance measurement
- Reference temperature applications
- Applications where small temperature errors are unacceptable
Four-wire measurement offers the best accuracy, but it is not automatically the best choice for every industrial installation.
PT100 Two-Wire vs Three-Wire vs Four-Wire
| Comparison | Two-Wire | Three-Wire | Four-Wire |
|---|---|---|---|
| Wiring complexity | Very simple | Moderate | More complex |
| Lead wire compensation | None | Partial compensation | Almost complete compensation |
| Measurement accuracy | Basic | Good | Highest |
| Typical cable distance | Short | Medium to long | Long |
| Installation cost | Lowest | Medium | Highest |
| Typical application | Basic equipment monitoring | General industrial processes | Laboratory and critical measurement |
| Industrial use | Limited | Most common | Special applications |

How to Select the Correct PT100 Wiring Method
Before selecting a PT100 configuration, check the following factors.
1. Check the Required Accuracy
For basic monitoring where a small temperature error is acceptable, two-wire may be sufficient.
For standard industrial control, three-wire normally provides a good balance between accuracy and cost.
For calibration, laboratory or critical process measurement, four-wire is generally preferred.
2. Check the Cable Distance
Longer cables have higher resistance.
For short cable runs, the error from a two-wire sensor may remain acceptable.
For medium or long distances, use a three-wire or four-wire configuration.
3. Check the Input Module
The PT100 wiring must match the input type of the PLC, DCS, temperature transmitter or indicator.
Do not assume that every RTD input supports all three wiring methods.
Check:
- Number of RTD input terminals
- Supported two-wire, three-wire or four-wire configuration
- Excitation current
- Sensor standard
- Input range
- Wiring diagram
4. Check the Installation Budget
Two-wire systems require less cable and fewer terminals.
Three-wire systems cost slightly more but provide much better practical accuracy.
Four-wire systems require additional cable cores and compatible input equipment.
5. Check the Process Importance
A small temperature error may be acceptable for equipment surface monitoring.
The same error may be unacceptable in:
- Calibration
- Chemical dosing
- Reactor temperature control
- Custody-related measurement
- Pharmaceutical production
- Laboratory testing
- Critical safety systems
Typical Application Recommendations
General Machinery and Equipment Monitoring
Recommended configuration:
Two-wire or three-wire
Two-wire may be acceptable for short-distance and non-critical measurements.
Three-wire is preferred when better stability is required.
Chemical and Process Plants
Recommended configuration:
Three-wire
Three-wire PT100 sensors are commonly used because they offer reliable accuracy at a reasonable installation cost.
Oil and Gas Applications
Recommended configuration:
Three-wire or four-wire
Three-wire is suitable for most process measurements.
Four-wire may be selected for critical monitoring, calibration or long-distance applications.
Power Generation
Recommended configuration:
Three-wire
Typical applications include bearing temperature, winding temperature, boiler systems and auxiliary equipment monitoring.
Laboratory and Calibration Systems
Recommended configuration:
Four-wire
Four-wire measurement is preferred where maximum accuracy and traceability are required.
Existing System Replacement
Recommended configuration:
Match the existing input and wiring definition first
Before replacing a PT100 sensor, confirm:
- Existing number of wires
- Terminal arrangement
- Sensor class
- Temperature range
- Cable length
- Input module type
- Probe dimensions
- Process connection
Do not select a replacement based only on the PT100 name.
Can a Three-Wire PT100 Be Connected as Two-Wire?
In some cases, a three-wire PT100 can be connected to a two-wire input by joining two matching wires.
However, the measurement system will then operate as a two-wire circuit.
This means the lead wire compensation advantage is lost.
The exact wiring arrangement should always be checked against the sensor and instrument wiring diagrams.
Can a Four-Wire PT100 Be Connected to a Three-Wire Input?
A four-wire PT100 may sometimes be connected to a three-wire input by joining two wires at one side of the sensing element.
However, the system will only provide three-wire compensation.
It will not retain the full accuracy advantage of a true four-wire measuring circuit.
Before changing the wiring, confirm that the wire pairs have been identified correctly.
Does More Wire Always Mean Better Performance?
Not necessarily.
A four-wire PT100 provides the highest potential accuracy, but it may not improve the overall process measurement if other errors are larger.
These may include:
- Incorrect sensor insertion depth
- Poor thermowell contact
- Slow response time
- Temperature gradients
- Transmitter accuracy
- Input module accuracy
- Process vibration
- Heat conduction through the sensor stem
The best configuration is the one that matches the actual accuracy requirement, installation distance, budget and input equipment.
Frequently Asked Questions
Which PT100 wiring method is most commonly used in industry?
Three-wire PT100 sensors are the most commonly used in industrial applications because they compensate for most lead wire resistance while keeping the wiring and equipment cost reasonable.
Is a four-wire PT100 always more accurate?
A four-wire PT100 provides the best compensation for lead wire resistance. However, total measurement accuracy also depends on the sensor class, transmitter, input module, installation and process conditions.
How much error can a two-wire PT100 produce?
The error depends on the resistance of both lead wires. Longer, thinner or warmer cables normally create more resistance and therefore more temperature error.
Can I replace a two-wire PT100 with a three-wire PT100?
It may be possible, but the input instrument must support three-wire RTD measurement. The terminal definitions and wiring diagram should be confirmed before replacement.
What information is needed to select a PT100 sensor?
Provide:
- Number of wires
- Temperature range
- Required accuracy
- Probe diameter and length
- Process connection
- Cable length
- Sensor class
- Head or cable type
- PLC, DCS or transmitter input
- Hazardous-area requirements
Need Help Selecting the Correct PT100?
Send us the existing sensor nameplate, wiring photo, probe dimensions and PLC or transmitter input details.
JCSCMRO can help verify the PT100 configuration, identify a compatible replacement and provide the correct sensor for your application.